Guangzhou NW Medical Co., Ltd. is a globally recognized leader in the design, manufacturing, and distribution of high-quality single-use sterile medical devices. We specialize in advanced solutions for infection control and surgical safety, with an unwavering commitment to enhancing the standard of patient care worldwide.
Our company is dedicated to providing OEM & ODM services for healthcare providers, distributors, and brand owners across the globe. With a focus on innovation, quality, and customer satisfaction, we ensure that our products meet the highest standards of safety and efficacy.
At Guangzhou NW Medical, we excel in integrating cutting-edge research and development with practical clinical applications, pushing the boundaries of medical technology.
Backed by extensive clinical data, our products are trusted worldwide, holding international compliance certifications including FDA, CE, and ISO standards.
Our products are engineered with a focus on reliability, clinical ergonomics, and exceptional patient outcomes, backed by a dedicated global support team.
We offer a wide range of single-use sterile medical devices and clinical consumables designed for safety and efficiency.
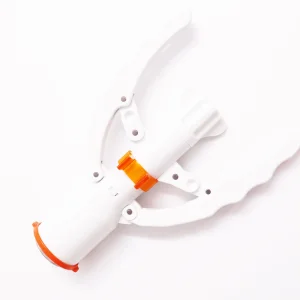
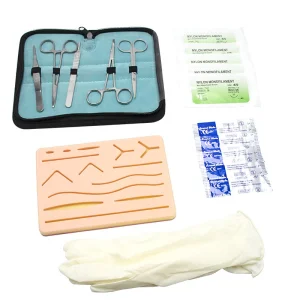
Precision-crafted single-use surgical apparatus designed for optimal tactile feedback and maximum surgical safety.
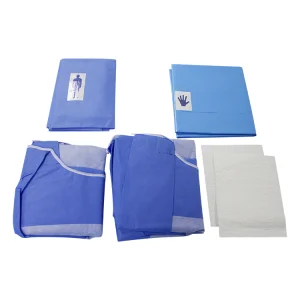
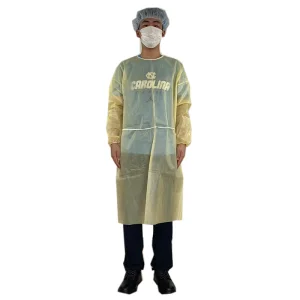
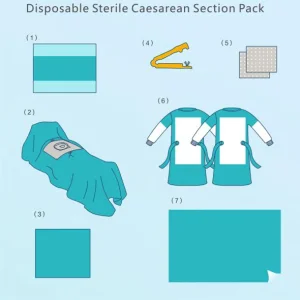
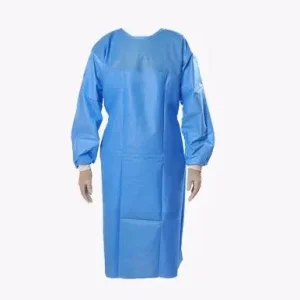
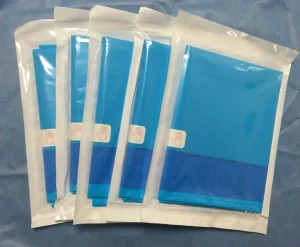
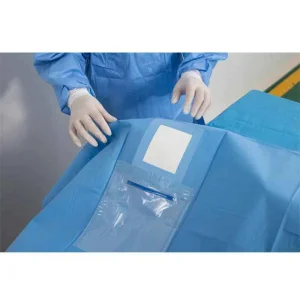
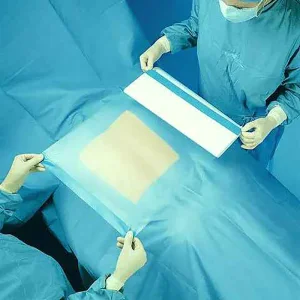
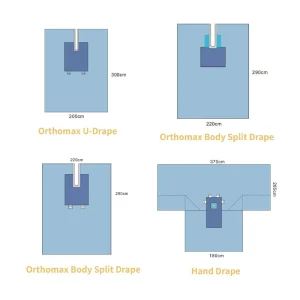
Advanced sterile drapes, gowns, and barrier kits to maintain sterile fields and prevent cross-contamination.
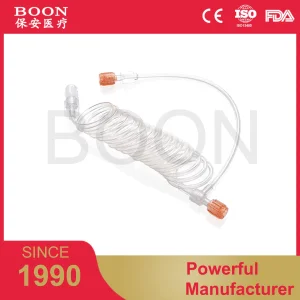
High-pressure medical tubing, coiled patient lines, and diagnostic peripherals engineered for accurate readings.
Our medical devices have established a proven track record across international healthcare institutions.
Successful Procedures Worldwide
Instrumental in improving clinical outcomes and patient recovery times across diverse specialties.
Sales Growth Over Three Years
Driven by enduring surgeon trust and verified clinical efficacy in reducing procedural risks.
Our team provides expert consultations, offering tailored solutions, technical documentation, and strategic guidance to meet your specific regulatory requirements.
We ensure smooth onboarding with seamless product integration into your facility's supply chain, supported by proactive account management.
Long-term partnership supported by responsive assistance, professional training, continuous product optimization, and a robust feedback loop.
Our upcoming research roadmap focuses on advanced bio-compatible ophthalmic irrigation fluids. By optimizing pH levels and electrolyte balance to closely mirror human tears, our sterile eye wash solutions will deliver instantaneous soothing comfort while neutralizing chemical ocular hazards in hazardous industrial and surgical environments.
Integrating intelligent sensor technology into emergency eyewash stations and portable sterile pods. Real-time telemetry will track expiration dates, fluid levels, and station activation status, ensuring 100% compliance with international workplace safety standards (ANSI/ISEA Z358.1).
Heavy chemical processing, semiconductor fabrication, and laboratory setups requiring immediate, reliable emergency decontamination.
Operating theaters and emergency departments requiring sterile irrigation during accidental chemical splashes or micro-debris exposure.
First responder kits and mobile trauma units equipped with compact, highly reliable single-use sterile eye wash ampoules and pods.
Navigating global medical device regulations requires rigorous paperwork. We provide comprehensive technical files, CE technical dossiers, FDA registration support, and biocompatibility testing reports to accelerate market entry in the EU, North America, LATAM, and APAC regions.
Flexible localization services including multilingual labeling, customized packaging design tailored to regional safety standards, and bespoke formulation adjustments to meet specific tender and hospital group purchasing organization (GPO) criteria.
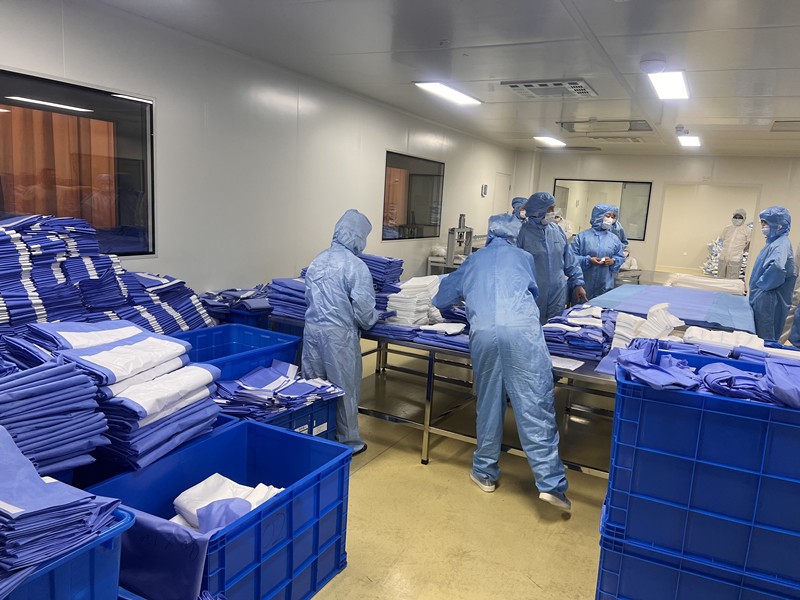
State-of-the-art Class 100,000 and Class 10,000 cleanroom facilities equipped with automated blow-fill-seal (BFS) technology for aseptic liquid packaging.
High-volume manufacturing lines ensuring buffer stock capabilities, mitigating global supply chain volatility and guaranteeing on-time delivery for enterprise partners.
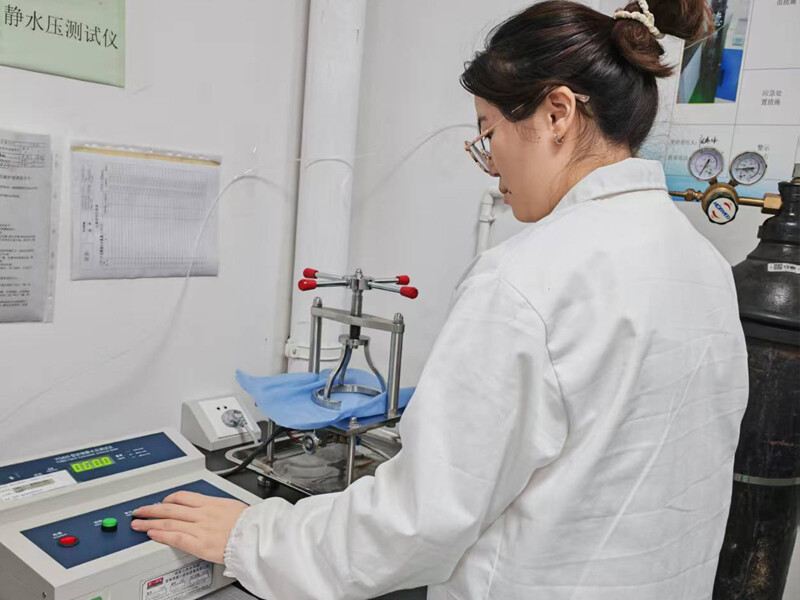
Rigorous inline optical inspection systems and automated sterility testing protocols ensuring absolute product safety before batch release.
With over 50,000 successful procedures globally, our products have been rigorously tested in real-world clinical environments.
Our products feature patented innovations that enhance both safety and efficiency in critical medical and emergency procedures.
From pre-sales consultations to ongoing after-sales support, we are committed to partnering with you at every step.
Our manufacturing aligns with international benchmarks including FDA and CE, ensuring uncompromised safety and trust.
We offer personalized product engineering and flexible manufacturing contracts tailored precisely to your brand specifications and regional market demands.
Our eye wash solutions are manufactured in ISO-certified cleanrooms using automated blow-fill-seal technology. They comply with stringent international standards, feature balanced pH isotonic formulations, and are backed by complete regulatory documentation including CE and FDA compliance support.
Yes. We specialize in comprehensive OEM and ODM partnerships. We provide custom bottle designs, tailored volumes, private label printing, multilingual packaging, and formulation adaptations to meet specific regional regulatory requirements.
MOQs vary depending on the product complexity and customization level. We strive to maintain flexible terms to support both emerging distributors and large-scale hospital group purchasing organizations. Please contact our sales engineering team for a tailored quotation.
Every production batch undergoes strict validation protocols, including automated leak testing, particulate inspection, and EO or aseptic processing sterilization validation in accordance with ISO 11135 and ISO 13485 standards.
 NW Medical